
Hey there! As a pipe body supplier, I've seen firsthand how these nifty components play a crucial role in the chemical industry. So, let's dive right in and chat about how pipe bodies are used in this dynamic field.
Transportation of Chemicals
One of the most fundamental uses of pipe bodies in the chemical industry is for transporting various chemicals. Chemicals come in all shapes and sizes - from corrosive acids to volatile solvents. Pipe bodies are like the highways that safely move these substances from one place to another within a chemical plant or even between different facilities.
We need to make sure that the pipe bodies we supply are made from the right materials. For example, when dealing with highly corrosive chemicals like sulfuric acid, we often recommend stainless - steel pipe bodies. Stainless steel has excellent corrosion resistance, which helps prevent leaks and ensures the long - term integrity of the piping system.
On the other hand, for less corrosive substances or those that operate at lower pressures, carbon steel pipe bodies can be a cost - effective choice. They are strong and can handle a fair amount of stress, making them suitable for many general chemical transportation applications.
Reactors and Process Equipment
Pipe bodies also play a key role in chemical reactors and other process equipment. In a chemical reactor, different chemicals are mixed and reacted under specific conditions of temperature, pressure, and time. Pipe bodies are used to introduce the reactants into the reactor and to remove the products.
Let's say we're talking about a polymerization reactor. Monomers are fed into the reactor through pipe bodies, and as the reaction takes place, the resulting polymer is then transported out of the reactor via other pipe bodies. These pipes need to be designed to handle the specific flow rates, temperatures, and pressures associated with the reaction.
Sometimes, pipe bodies are also used for heat exchange within the reactor. They can carry a cooling or heating fluid to control the temperature of the reaction. This is super important because the rate and outcome of a chemical reaction can be highly dependent on temperature.
Storage and Distribution
In chemical storage facilities, pipe bodies are used to connect storage tanks to other parts of the plant. For instance, when chemicals need to be transferred from a large storage tank to smaller containers for further processing or shipping, pipe bodies are the go - to solution.
They also help in distributing chemicals evenly throughout a plant. A well - designed piping network can ensure that each production unit gets the right amount of chemicals at the right time. This is crucial for maintaining consistent product quality and efficient production processes.
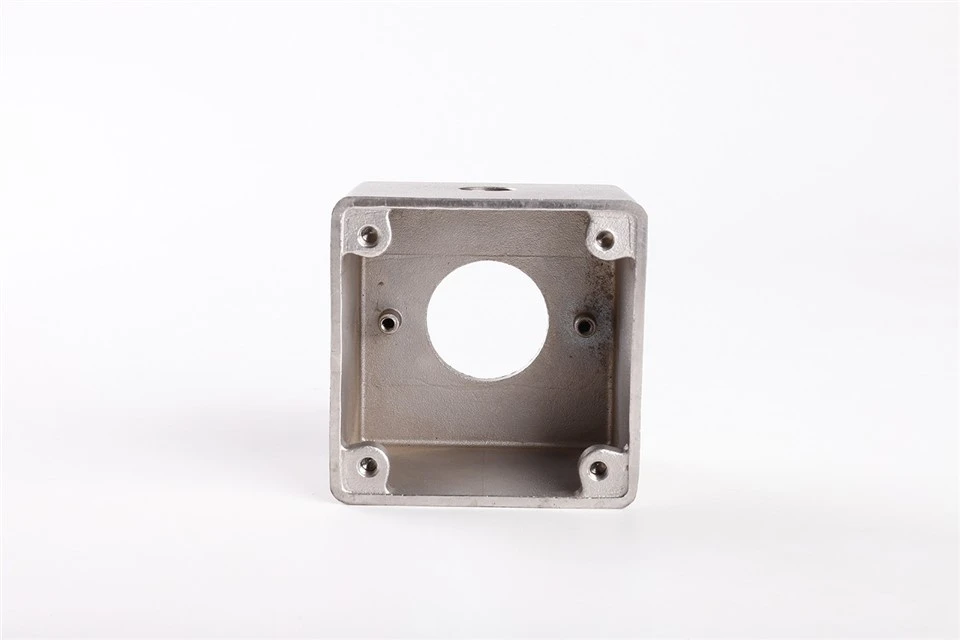
Let's take a look at some of the products that are related to pipe bodies in the fluid machinery parts category. You can check out the Ultrasonic Water Case, List Box, and Cup Cover. These products might not be pipe bodies themselves, but they are all part of the larger fluid machinery ecosystem that often works in tandem with pipe bodies.
Safety and Maintenance
Safety is a top priority in the chemical industry, and pipe bodies are no exception. We need to ensure that the pipe bodies we supply meet strict safety standards. This includes proper installation, regular inspection, and maintenance.

Regular inspections can help detect any signs of wear, corrosion, or damage early on. For example, ultrasonic testing can be used to check the thickness of the pipe walls and identify any potential weak spots. If a problem is detected, prompt maintenance or replacement of the pipe body can prevent a major accident.
Proper installation is also crucial. Pipe bodies need to be installed with the right supports and fittings to ensure that they can withstand the forces acting on them. Incorrect installation can lead to leaks, vibrations, and even structural failures.
Customization and Innovation
The chemical industry is constantly evolving, and so are the requirements for pipe bodies. That's why we, as a pipe body supplier, focus on customization. We work closely with our customers to understand their specific needs and design pipe bodies that are tailored to their applications.
For example, some chemical processes might require pipe bodies with special coatings to enhance their corrosion resistance or reduce friction. Others might need pipes with unique shapes or sizes to fit into a particular piece of equipment.
Innovation is also key. We're always looking for new materials and manufacturing techniques to improve the performance of our pipe bodies. For instance, the development of composite materials that combine the strength of metals with the corrosion resistance of polymers could open up new possibilities for chemical piping systems.
Conclusion
In conclusion, pipe bodies are an essential part of the chemical industry. They are used for transportation, in reactors and process equipment, for storage and distribution, and play a crucial role in safety and maintenance. As a pipe body supplier, I'm proud to be part of this industry and to contribute to the smooth operation of chemical plants around the world.
If you're in the chemical industry and are looking for high - quality pipe bodies, I'd love to have a chat with you. Whether you need standard pipe bodies or custom - designed solutions, we've got you covered. Reach out to us, and let's start a conversation about how we can meet your pipe body needs.
References
- Chemical Engineering Handbook, various editions
- Journals of Chemical Industry and Engineering, multiple issues
- Industry reports on chemical piping systems and safety standards